

Cradle Type Steel Wire Armoring Machine
The machine is mainly used for steel wire armoring of various types of cables, and also for bare copper and bare aluminum wires. The machine is mainly composed of pay off, stranding cages, die holder, taping device, meter counter, capstan, take up with traverse rack, transmission system and electrical control system, etc.
- Product Details
- Applications
- Technical Parameters
- RFQ & FAQ
Product Overview
The machine is mainly used for steel wire armoring of various types of cables, and also for bare copper and bare aluminum wires. The machine is mainly composed of pay off, stranding cages, die holder, taping device, meter counter, capstan, take up with traverse rack, transmission system and electrical control system, etc.
Structural Features And Configuration
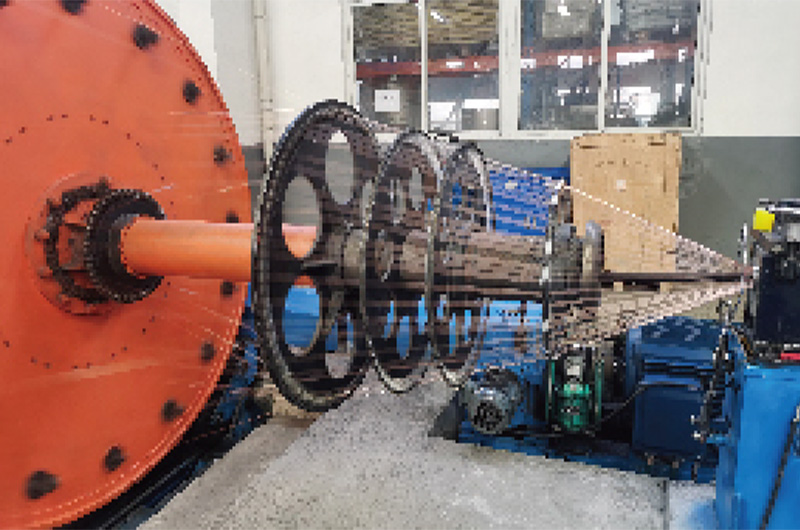
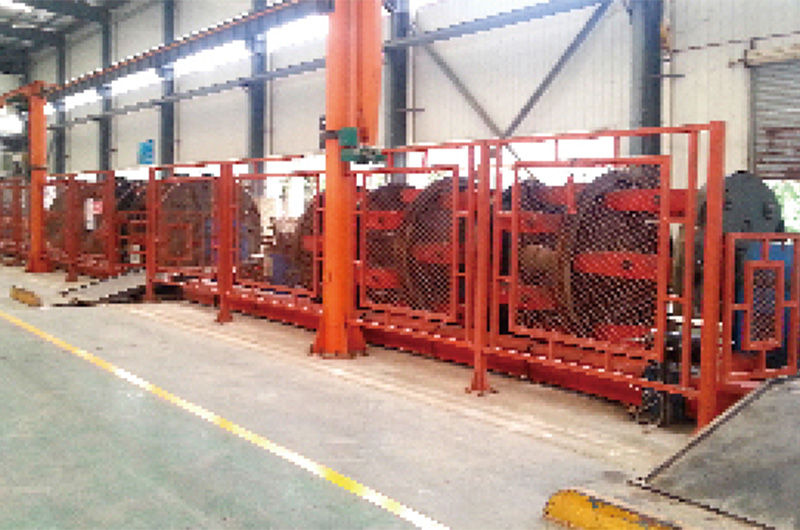
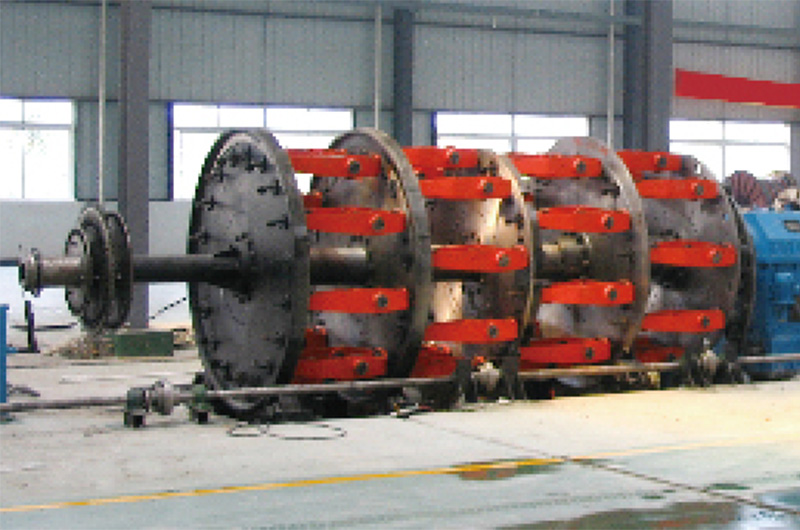
Heavy-duty cradle cages
The stranding cages adopt a "Cradle" structure. This robust design is specifically calculated to bear the weight of steel wire bobbins (typically 500mm or 630mm). The cages are rigid and durable, ensuring stable tension control for each individual steel wire.
Strong traction system
Armored cables are heavy and stiff. The line is equipped with a high-pulling-force traction device (Capstan or caterpillar) to ensure smooth cable movement without slippage.
Versatile taping integration
Non-metallic taping: For PET, non-woven, semiconductor tape and so on.
Steel taping device: For steel tape armoring.
Product Images And Drawings

Applications And Process Scope
Designed to support a wide range of wire and cable processing requirements with flexible drive and tension configurations.
Steel wire armoring: Applying a layer of galvanized steel wires around the cable bedding. Essential for multi-core power cables.
Bare conductor stranding: Twisting of large cross-section bare copper and aluminum wires
Screening: Applying copper wire screens for medium/high voltage cables.
Double armoring: With added taping heads, it can apply steel tape armoring in the same pass.
Technical Specifications
Technical data for the KLY-400/36+36, KLY-500/48+48, KLY-630/48+48 planetary stranding machine models.
| Type | KLY-400/36+36 | KLY-500/48+48 | KLY-630/48+48 |
|---|---|---|---|
| Single wire dia. (mm) | Steel: 0.5-2.5 | Steel: 0.8-3.5 | Steel: 1.0-3.5 |
| Copper: 1.0-4.0 | Copper: 1.0-4.0 | Copper: 1.0-4.0 | |
| Max. Stranded dia. (mm) | 80 | 100 | 120 |
| Cage rotation speed (rpm) | 20-46.3 | 16-38 | 13.2-31.4 |
| Stranding pitch (mm) | 95-1600 | 111-1938 | 133.7-2348 |
| Taping rotation speed (rpm) | 169-387 | 169-387 | 169-387 |
| Taping pitch (mm) | 11-189 | 11-183 | 11-183 |
| Traction force | Pneumatic 40KN | Pneumatic 50KN | Pneumatic 80KN |
| Traction speed (m/min) | 4.4-32 | 4.2-31 | 4.2-31 |
| Bobbin in the cage | PN400 | PND500 | PND630 |
| Central pay off | PN1250-PN2500 | PN1600-PN3150 | PN1600-PN3150 |
| Take up | PN1250-PN2500 | PN1600-PN3150 | PN1600-PN3150 |
| Main motor (kw) | 55 (AC) | 110 (AC) | 132 (AC) |
Frequently Asked Questions
Find answers to common questions about product selection, configuration and technical requirements.
Information required for quotation?
Intended product; material and input/output diameter; wire quantity, finished diameter, and required pitch; required speed; electrical supply and floor space.
How should the correct model be selected?
Match the required parameters to Section 5, then confirm the final configuration in a product-specific technical agreement.
Are optional or customized configurations included?
Only changes and optional devices expressly listed in the final technical proposal and supply scope are included.
Which values govern the final purchase?
Catalog data are transcribed from the supplied source; the signed technical agreement governs the final scope and values.

